FOR EXAMPLE
T70 3 PLY = EP125 3 PLY = 125 x 3 = CLASS 375
T112 3 PLY = EP200 3 PLY = 200 x 3 = CLASS 600
T140 4 PLY = EP250 4 PLY = 250 x 4 = CLASS 1000
CARCASS PLIES
These range from 2 to 6 ply and are either a polyester/nylon mix (EP) or nylon only (NN).
EP conveyor belts are preferred due to :
a. Less stretch than nylon belts;
b.Troughing capability thanks to flexibility.
Sealed edge conveyor belts protect the plies from moisture and separation.
GRADE OF COVERS
Different conveyor belt qualities or grades, suit particular applications.
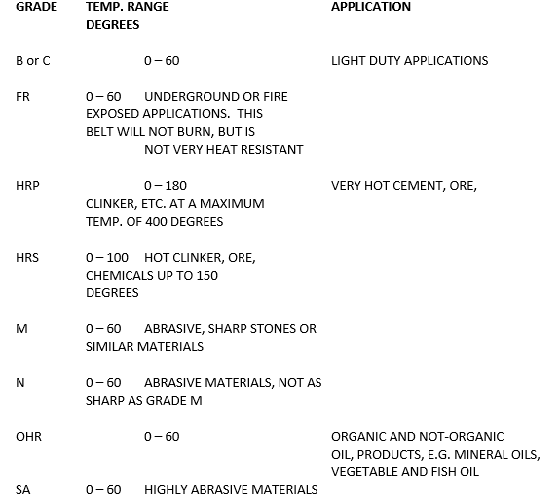
COVERS – TOP AND BOTTOM
a) TOP COVER
This protects the carcass plies from material damage. Abrasive, sharp stones falling onto a belt will need a 5mm or greater top cover, while belts carrying softer materials need only have a 3mm top cover. Minimum 2mm, maximum 10mm.
b) BOTTOM COVER
This protects the carcass plies from the conveyor bed rollers and guides, and prevents wet material build up on the underside of a belt. Similar to the top cover, abrasive materials will require a bottom cover of up to 5mm; while the normal thickness is 1.6mm.
STEEL CORD CONVEYOR BELTS
These conveyor belts have many high tensile, steel cords running lengthwise through the belt instead of carcass plies. This offers:
a) Extreme high tensile strength, up to 5000 kg/cm;
b) Minimal belt stretch for long conveyors;
c) Good tough ability and impact resistance.
Steel cord belts are most suited to extra-long belt systems, e.g. 1km drives, carrying heavy materials on a troughed conveyor. Hwange Colliery, Zisco Steel and some large mines with inclining main shafts would require these conveyor belts.